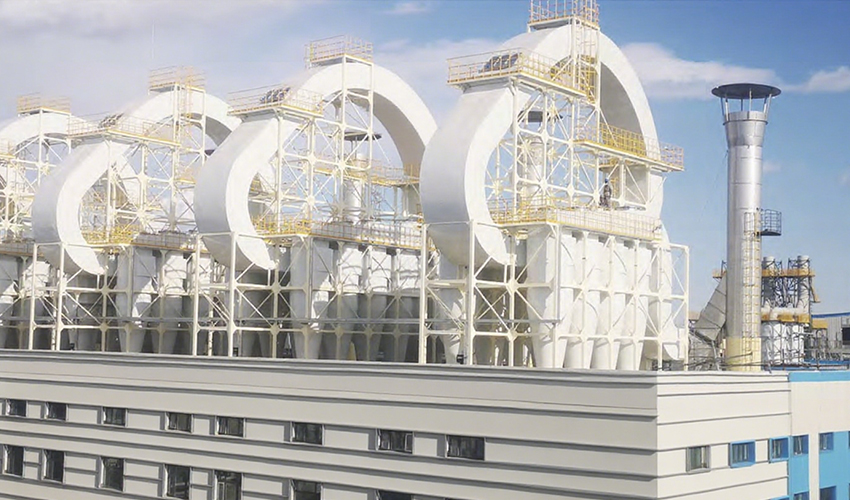

A fuel ethanol plant can run, or it can respond. The difference shows in steam flow, fermentation temperature, molecular sieve timing, and the speed at which operators isolate a process upset. An ethanol plant control system is not an accessory layer bolted onto process units. It is the operational backbone that decides whether a plant reaches intelligent manufacturing or continues running as a collection of automated islands. In our corn-to-ethanol project work, we treat DCS design as the integration layer for energy, byproduct, and quality decisions, not as a late-stage wiring exercise.
What Does an Ethanol Plant Control System Need to Control First?
Material balance comes before device count. In a corn-to-ethanol plant, the control system has to hold the front end together: grain receiving, cleaning, milling, slurry makeup, liquefaction, saccharification, fermentation, distillation, dehydration, evaporation, and dryer performance. Each unit affects the next. If the mash feed rate drifts, downstream steam demand drifts with it. If the beer column feed loses temperature, the rectifier sees a different composition profile and the molecular sieve cycle shortens. A control system that only automates individual pumps will not run the process; it will only display it.
| Control domain | Primary control objective | Integration point | Common failure mode |
|---|---|---|---|
| Grain receiving and milling | Moisture and particle size consistency | Front-end throughput and slurry density | Silo segregation with no corrective routing |
| Liquefaction and saccharification | Enzyme contact time and temperature profile | Steam supply and mash viscosity | Temperature overshoot that deactivates enzyme |
| Fermentation | Heat rejection and yeast activity | Cooling water and CIP sequence | Local temperature drift lowering yield |
| Distillation and dehydration | Stable column pressure and reflux | Steam network and molecular sieve cycle | Pressure swings shifting azeotrope operation |
| Byproduct and utility recovery | Energy and mass reuse | DDGS drying, CO2, biogas, wastewater | Uncoordinated utility and process loads |
Why Is Fermentation Control Harder Than Distillation Control?
Fermentation is a biological loop with a long response time. A change in mash concentration or cooling water temperature may not show up as a yield shift for several hours. Distillation, by contrast, reacts to pressure, level, and reflux changes within minutes. A DCS that handles both must combine slow feedforward models for fermentation with fast multivariable loops for the distillation train. If the two are tuned as though they behave the same way, operators end up chasing one variable and disturbing the other.
How Should Molecular Sieve Switching Be Sequenced?
Molecular sieve beds switch between adsorption and regeneration on a strict time or differential pressure schedule. The DCS sequence has to coordinate feed valves, regeneration gas flow, heating, cooling, and depressurization without sending a pressure pulse back into the rectifier. In our project reviews, we look for sequence narratives that define each transition state, not just a valve list. A missing state in the sequence is a common source of purity trips during commissioning.
Why Is DCS Architecture Still the Core of an Ethanol Plant Control System?
Intelligent manufacturing does not replace DCS architecture; it depends on it. A distributed control system keeps loop execution, alarm handling, and interlock logic close to the process, while a SCADA layer on top of standalone PLCs often turns every process area into a separate data island. For ethanol production, where distillation and dehydration can interact in minutes, that difference matters. DCS controllers run deterministic control functions at the process level, which preserves loop integrity even when the plant network or HMI server is under load.
A modern DCS also carries the data spine for higher-level applications: advanced process control, real-time optimization, batch reporting, energy management, and maintenance analytics. A plant that treats the DCS as a wiring and loop project will later find that intelligent manufacturing requires rebuilding the data structure. A plant that treats the DCS as the operational data model can deploy optimization without a separate historian retrofit.
How Do Energy Cascade and Byproduct Streams Change Control Requirements?
A fuel ethanol plant is also an energy plant and a byproduct plant. Stillage from the distillation train goes to DDGS drying or biogas recovery. Carbon dioxide from fermentation can be captured. Condensate and low-pressure steam can be reused across evaporation and cook systems. The control architecture has to treat these streams as part of the same heat and mass balance, not as downstream add-ons.
AGRIFAM’s corn deep processing reference design uses intelligent digital control with a 25 percent energy consumption reduction target and full byproduct resource utilization in a corn-food-energy-feed loop. The same systems view applies to alcohol production: if stillage flow drops because fermentation yield drops, the DDGS dryer and biogas feed lose stability unless the control system anticipates the change. If the molecular sieve regeneration steam demand rises, the steam header and evaporation load should respond together.
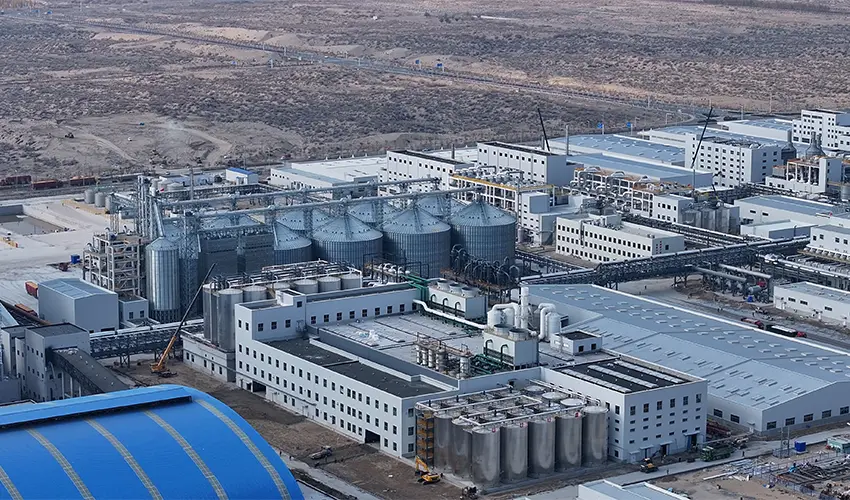
If your ethanol plant includes multi-effect evaporation, molecular sieve regeneration, or biogas recycle, it is worth confirming whether the control architecture handles those as one energy network rather than separate utility packages before you finalize the BOM. Send your process flow and integration scope to [email protected].
What Makes a Control System Procurement Specification Fail?
Most failed control system specifications do not fail because they are too short; they fail because they specify hardware instead of behavior. A document that lists cabinet sizes, I/O counts, and network switches gives vendors nothing about how the loops should work together. The useful specification starts with control narratives, alarm rationalization, interlock matrices, batch sequences, and interface responsibilities. I/O count follows from those, not the other way around.
Should the Specification Start with I/O Count or Process Function?
Start with process function. I/O count is a downstream consequence of the control strategy. A fermentation train with redundant temperature loops and automatic CIP sequences will have a different I/O profile than a simple level and pump control installation. If the specification fixes I/O count first, the vendor is forced to design the process logic around the hardware budget, which usually shows up as missing instruments or overworked control loops during commissioning.
How Do You Avoid a System That Is Obsolete Before Commissioning?
The main risk is buying a platform with no upgrade path for advanced process control, no open historian interface, and no clear alarm management workflow. Ask the vendor to show native OPC UA, batch management, and historian interfaces. Then require the same platforms to be demonstrated on a reference ethanol or grain processing plant. A control system that cannot carry real-time process data to an APC or energy management layer becomes a retrofit problem within the first operational year.
When Should the Ethanol Plant Integration Architecture Be Locked Before Procurement?
The integration architecture has to be locked before major equipment orders, not after. Once pumps, heat exchangers, columns, dryers, and utility packages have been purchased, the upstream and downstream control interfaces are partly fixed. Waiting until construction to define DCS interface points leads to hardwired fallbacks, serial links, and operator workarounds.
Locking the architecture means agreeing on control boundaries between package skids and the central DCS, the type of remote I/O, the historian structure, alarm priorities, and cybersecurity zones. For an ethanol plant, it also means deciding how the plant will operate during molecular sieve regeneration transitions, CIP, and partial load.
The pain point is not that control systems are difficult to buy; it is that correcting an integration gap after commissioning costs more than getting the architecture right before procurement. AGRIFAM supplies grain-based alcohol and fuel ethanol EPC solutions that carry the control philosophy through from process design to commissioning, so the DCS architecture aligns energy cascade, byproduct recovery, and intelligent manufacturing as one system. Send your PFD, I/O list, and control narrative to [email protected] or call 010-8591 2286, and we will work through the integration sequence for your corn-to-ethanol configuration.
What Else Should Buyers Ask Before Selecting a Control System Partner?
Is a DCS Overkill for a Smaller Ethanol Plant?
Not if the plant runs continuous distillation and dehydration. A smaller plant may use a compact DCS or a hybrid PLC and SCADA system, but the control strategy still has to manage column pressure, reboiler duty, and molecular sieve switching as coordinated sequences. The key question is not total I/O count; it is whether the platform can execute those sequences under one alarm and historian model. If the answer is no, the savings from a lower-cost PLC system usually disappear during commissioning and operation.
How Much Should a Control System Vendor Know About Ethanol Process Technology?
It is a mistake to treat the control system vendor as a hardware supplier only. Ethanol dehydration, stillage handling, and energy recovery create control problems that generic manufacturing platforms do not see. A vendor with only building automation or batch food experience may miss the interaction between fermentation cooling and distillation steam load. Ask for a proven reference in fuel ethanol or grain deep processing. The platform matters less than the vendor’s ability to write control narratives that match your PFD.
What Happens If the DCS Sequencing Is Not Fully Defined Before Commissioning?
In projects where the DCS sequencing is left vague, startup follows a predictable pattern: water batching runs, then process interlocks are added under schedule pressure, then operators create manual workarounds for sequences the system cannot handle. In our experience, the control narrative has to be complete before loop checks begin. If your project has multiple package vendors or a new molecular sieve unit, it is worth confirming the sequence ownership before commissioning. Share your process flow and control philosophy, and we will confirm whether the integration scope matches your corn-to-ethanol configuration.
If you’re interested, check out these related articles:
Driving Global Food Conservation Through Technological Innovation