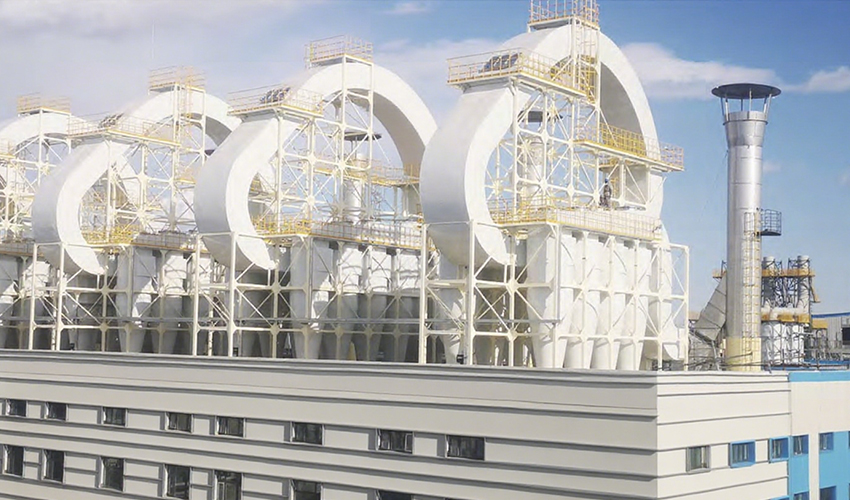

Most ethanol plant operators do not fear the corn itself. The real hazard forms in dust that escapes during receiving, conveying, cleaning, and milling, then settles on beams, floors, and equipment. Ethanol plant dust explosion prevention succeeds when that dust is controlled before it can form an explosive cloud and when ignition sources are removed from the same spaces. In our grain alcohol and fuel ethanol project work, I have seen the same pattern: plants that engineer dust control into material flow need far less suppression and intervention later.
Corn Dust in an Ethanol Plant Can Explode Before a Front-Line Operator Sees It
Corn dust is a combustible dust, and in an ethanol plant it is produced at nearly every transfer point. A single kernel drop creates fines, and repeated handling concentrates the smallest particles in enclosed spaces. The explosion pentagon adds dispersion and confinement to the familiar fire triangle. A bucket elevator, an enclosed drag conveyor, or a silo headspace can supply both. I look first at transition points between receiving, cleaning, and grinding because that is where dust clouds form and where pressure can build if ignition occurs.
| Hazard factor | What creates risk | What to check in design |
|---|---|---|
| Dust particle size | Fines small enough to remain suspended disperse quickly and ignite with less energy | Screening and aspiration at transfer points |
| Dust concentration | A cloud below visible limits can still exceed the minimum explosible concentration | Airflow design and dust collection at containment boundaries |
| Enclosure geometry | Bucket elevators and silo heads can confine pressure | Explosion venting and isolation layout |
| Moisture content | Dry fines from milling and cleaning become more dispersible | Moisture control without creating flow blockages |
| Ignition sources | Bearings, static, welding, and electrical faults appear in normal operation | Bearing temperature monitoring and hot work controls |
Source Dust Control Changes the Risk Profile of the Entire Grain Handling Circuit
Prevention starts before dust reaches a filter. We design grain receiving and conveying systems with source aspiration and sealed transfer chutes, because removing dust at the point of generation keeps it from accumulating inside enclosures and on structural steel. A well placed aspirator or dust collection pickup near the receiving pit and bucket elevator boot reduces the fugitive dust load that later becomes a housekeeping burden. The same logic applies to cleaning. Rotary screens and magnetic separators should sit upstream of milling to remove fines and tramp metal before they create an ignition risk.
Why bucket elevators and drag conveyors become early explosion points
Legs are the most common source of grain dust explosions because they combine moving parts, fine dust, and an enclosed casing. Bearing heating inside a bucket elevator can raise dust to its ignition temperature while the casing provides confinement. We specify bearing temperature sensors and vibration monitoring on legs wherever dust and hot surfaces could meet, and we keep the boot and head sections accessible for inspection rather than sealed away.
What receiving pit dust collection must handle
Receiving pits collect corn fines, soil, and broken kernels, so the dust control system must manage both airborne dust and heavier material. A dust pickup at the pit discharge alone is not enough. The aspiration hood needs to capture dust released when corn strikes the grate and when the receiving conveyor starts and stops, which is often where fugitive dust escapes.
Housekeeping Is Where Ethanol Plant Dust Explosion Prevention Programs Succeed or Fail
Suppression and venting do not remove the fuel. Fugitive dust on floors, beams, and ledges is the fuel source that turns a small fire into a deflagration. I have walked through plants where the baghouse was well maintained, yet enough dust had settled on overhead conduit to carry flame across an entire room. That gap is not an equipment failure. It is a housekeeping failure. Written cleaning schedules fail when they are not tied to specific surfaces and frequencies. The surfaces that matter most are hidden: cable trays, beam flanges, equipment tops, and the area around elevator heads. A housekeeping plan that only covers floors will not reduce explosion risk.
Why fugitive dust accumulation changes the risk calculation
Even a thin dust layer can become an explosive cloud when a primary explosion shakes it loose. That is why NFPA standards treat housekeeping as an engineering control, not a janitorial task. In our project reviews, we treat visible dust accumulation as evidence that a transfer point or ventilation hood is underperforming. We then trace the source and correct the airflow rather than only scheduling another cleaning pass.
What a realistic cleaning schedule covers
A practical schedule names every surface, assigns a maximum dust depth, and sets the frequency that keeps dust below that depth. High traffic areas around receiving and milling may need daily attention. Overhead surfaces can be cleaned weekly or monthly if source controls are effective. The schedule should also specify tools that do not create static or sparks, because vacuum cleaners and compressed air lines can become ignition sources themselves.
If your plant handles corn with a wide moisture range, the dry season is the right test condition for housekeeping frequency and duct velocity. Send your floor plan and current dust collection layout to [email protected], and we will confirm whether your cleaning intervals and conveying velocities match the dust load your process creates.
Ignition Source Control Closes the Explosion Pentagon
Controlling fuel is half the job. A combustible dust cloud without an ignition source cannot explode. In grain handling, the most dangerous ignition sources are not dramatic. They are overheated bearings, misaligned belts, static discharge, and hot work. Bearing temperature sensors should be installed on bucket elevator legs, conveyors, and fan shafts, with alarms that stop the leg before temperatures reach dust ignition ranges. Static bonding and grounding matter because flowing corn and dust can generate enough charge to spark. Flexible hoses, filter bags, and isolated metal sections all need a defined grounding path.
Hot work permits are a management control that works only when they include a dust inspection of the surrounding area before work starts. A welder cutting into an idle conveyor can ignite dust that has been sitting in the casing for weeks. We require a documented clean zone around hot work and a fire watch after the work stops, because smoldering dust can transition to flame long after the spark.
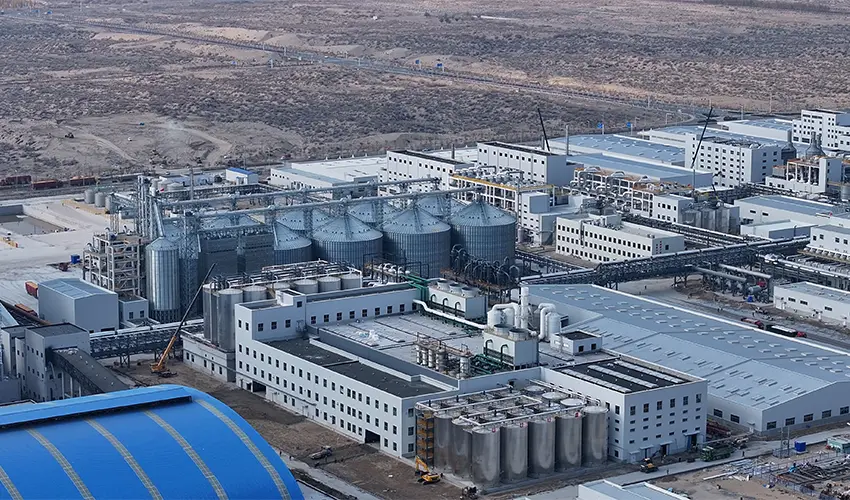
Explosion Protection Design Completes an Ethanol Plant Dust Explosion Prevention System
Source control, housekeeping, and ignition management reduce probability. Explosion protection addresses what happens if prevention fails. Vent panels, explosion isolation, and suppression are not substitutes for dust control; they are the last line of defense. A vented bucket elevator leg still releases flame and pressure into the building unless the vent is directed to a safe area and the connected ductwork is isolated. Isolation devices, usually chemical isolation or a mechanical barrier, stop a deflagration from traveling back into the receiving pit or forward into a silo. These systems need an engineering review that matches the dust Kst and Pmax values of the actual corn fines being handled. Generic designs based on a different dust class can fail exactly when they are needed.
Design is only half the commitment. Vent panels that are painted shut, isolation valves that are not inspected, and suppression canisters past their service date create a false sense of protection. I often see plants where explosion protection exists on the drawings but no longer works in the field. Maintenance of these systems belongs in the same work order schedule as the process equipment. A plant should not run a hammer mill or a bucket elevator leg while its explosion isolation is out of service.
Most ethanol plant safety gaps do not come from missing alarms. They come from grain handling flows that were not designed with dust control as a governing parameter, and from housekeeping routines that drift once production pressure rises. AGRIFAM can review your receiving, conveying, cleaning, and dust collection layout against your current risk profile and recommend the few changes that create the largest safety return. Send your plant layout and dust hazard analysis summary to [email protected] or call 010-8591 2286, and we will confirm the highest-priority corrections for your specific grain handling circuit.
Ethanol Plant Dust Explosion Prevention Questions Come Up in Every Project
What dust concentration is actually explosive in an ethanol plant?
Operators cannot wait until a dust cloud looks thick. The minimum explosible concentration for corn starch and corn dust is far below the point where vision becomes limited, so a cloud that looks like a haze can already support a deflagration. The exact value depends on particle size, moisture, and oil content, which vary between incoming corn lots. For this reason, we design around the driest, finest material a plant expects to handle. If your grain streams change seasonally, your dust control basis should be checked against the worst case, not the average.
Can a baghouse dust collector stop an ethanol plant dust explosion?
A dust collector removes suspended dust, but it does not remove the fuel already settled inside a bucket elevator leg or on structural steel. Many operators assume the baghouse is the primary explosion safety system. It is not. A baghouse controls emissions and reduces housekeeping load; it still needs explosion venting or isolation because the filter itself contains dust clouds. The real prevention step is source capture at transfer points. A plant with a large baghouse and poor hood placement can still have dangerous dust releases.
How often should fugitive dust be cleaned in grain handling areas?
It depends on the dust fall rate and the surface. Around receiving and milling, dust may reach unsafe depths daily during dry corn campaigns, so these areas need daily or shift-based cleaning. Overhead beams and conduit that collect dust slowly can be cleaned weekly or monthly when source capture is effective. The controlling metric is not time alone. It is the measured dust depth that can be lofted by a primary explosion. We set limits by surface type and inspect with a written checklist, not by memory.
Is a dust hazard analysis required before changing grain handling equipment?
Any dust hazard analysis should be updated when the process flow changes. In our project reviews, a dust hazard analysis is useful only when it follows the current process. If you add a receiving pit, change a conveyor route, or start handling a different corn grind, the dust sources, confinement points, and ignition risks change with it. Running new equipment on an old analysis leaves blind spots. If you are planning a silo or conveyor change, send your flow diagram and current dust collection points to [email protected] and we will confirm whether your dust hazard analysis covers the new configuration.
If you’re interested, check out these related articles:
Driving Global Food Conservation Through Technological Innovation