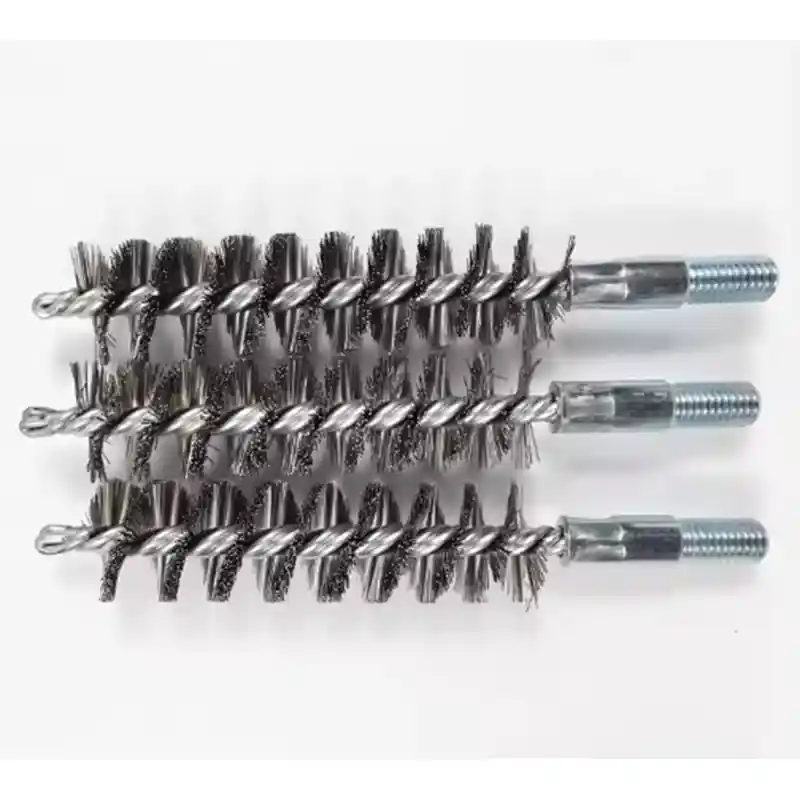

Wire pipe brush selection fails on the details that are not visible in catalog photos: stem length, fill density, wire hardness, and the fit between brush OD and pipe ID. A brush that is too dense stalls a hand drill; a stem that is too thin snaps at the pipe opening; a fill that is harder than the tube wall leaves scoring that becomes a corrosion site. This article explains how to specify these details for industrial pipe inner wall cleaning, rust removal, and deburring without spending on trial samples that do not survive the first bore.
What a Wire Pipe Brush Does Inside a Pipe
A wire pipe brush cleans by rotary contact rather than by abrasion from a flat face. The stem turns a twisted fill of wire, and each wire tip strikes the bore at a slight angle. That action breaks rust, light scale, carbon staining, and burrs free from the pipe wall without removing significant base metal. It is not a honing tool, and it should not be expected to open an undersized hole or correct an out-of-round pipe.
We use two decisions to describe a wire pipe brush before quoting: the work it needs to do and what the bore condition can accept. If the pipe is straight and the deposit is old carbon steel scale, a denser carbon steel fill with a stiffer stem works. If the same brush runs in a copper or aluminum tube, that same carbon steel fill can gouge the wall. The cleaning mechanism is simple; the specification is not.
Wire Pipe Brush Specifications That Change Performance
Four measurements control how a wire pipe brush behaves in a bore: brush outside diameter, trim length, fill wire diameter, and stem diameter. Brush OD determines interference. For most straight steel pipes, we specify the brush OD 3 to 5 mm over the nominal pipe ID so the wire tips press into the wall without flattening. The trim length, meaning the axial length of exposed fill, controls how much of the bore is engaged in one pass. A short trim follows the pipe line better; a long trim cleans more area but loads the stem harder.
Stem diameter is the most common failure point in short run production. A 6 mm stem is fine for a 150 mm pipe, but the same stem becomes unstable in a 700 mm bore because the overhang magnifies vibration at the collet. The fill wire diameter then sets how aggressively the tips cut. Lighter wire, around 0.15 to 0.25 mm, flexes more and suits deburring or light rust. Heavier wire, around 0.30 to 0.50 mm, resists breaking on scale but transfers more load to the tube wall.
Fill Material Selection Against Pipe Condition and Base Metal
Fill material should be matched to both the deposit and the tube material. Carbon steel fill is the workhorse for steel pipe with rust, mill scale, or cementitious residue. Stainless steel fill makes more sense for stainless tubes, food contact lines, or wet environments where carbon steel particles left behind can start corrosion. Brass fill is the non-sparking choice for softer metals and for cleaning without cutting into aluminum, copper, or thin stainless.
Brass fill is the default for pipe IDs where sparking must be avoided or where the tube base metal is softer than carbon steel. <brass brushes work perfectly for pipe cleaning> covers why brass wire removes deposits without cutting into copper, aluminum, or stainless tube walls and where brass becomes the wrong choice once heavy scale covers the bore.
Nylon abrasive fill fits a different job. It cannot remove deep rust, but it can deburr drilled intersections, break sharp edges, and remove light carbon without changing the bore dimension. When we see a deburring request where the drawing tolerance is tight, we move to a flexible nylon or fine stainless fill before a carbon steel fill because the risk of dimensional change is lower.
| Fill material | Pipe condition | Base metal fit | Main risk |
|---|---|---|---|
| Carbon steel | Rust, heavy scale | Steel, cast iron | Bore scoring if overdriven |
| Stainless steel | Rust, scale, wet service | Stainless, alloy steel | Higher cost, harder on soft metals |
| Brass | Light oxidation, carbon | Copper, aluminum, brass | Short life on heavy scale |
| Nylon abrasive | Light burrs, edge break | Most metals | Cannot remove thick deposits |
Stem Life and Operating Speed on Wire Pipe Brushes
Speed is set by brush OD and overhang, not by what the drill can reach. A small wire pipe brush of 10 mm OD can run near 1,500 RPM because the tip mass is low. A 50 mm brush at that speed throws the fill outward and beats the stem into the pipe mouth. We normally start with the lower third of the common drill range, then increase only if the fill does not bog down. For a 20 to 25 mm carbon steel fill brush, 500 to 1,000 RPM is a reasonable starting point in steel pipe.
Stem whip is the more destructive failure because it happens at the pipe opening before the fill wears out. The unsupported stem section between the collet and the pipe face is the weak zone. If the pipe entry is narrow or the collet sits more than 100 mm back, even a straight run will oscillate. That oscillation flexes the stem until it hardens and snaps. In those cases we specify a shorter trim, a larger stem, or a reinforced double stem with a gradual taper at the transition.
When scale builds to the point that a single wire pipe brush cannot drag it free, a spiral brush with inward or outward twist changes the attack angle. <descaling spiral brush an innovative tool and generalist in the field of industrial cleaning> covers how twisted stem construction holds heavier fill and feeds debris along a defined path, which matters on long pipe runs.
If your program involves bores over 800 mm, multiple bends, or a clamp distance that forces long overhang, confirm stem construction before freezing the drawing. Send the pipe ID, depth, and material to [email protected] and we will confirm whether a standard wire pipe brush will run or whether a custom stem extension is required.
Wire Pipe Brush Details to Confirm Before Ordering
Most wire pipe brush rejections in our work come from a drawing that specifies only OD and wire material. That is enough for cleaning a short, straight, open pipe. It is not enough for a pipe with a shoulder, a bend, a blind hole, or a wall material that is softer than the fill.
We check six items before quoting: minimum and maximum pipe ID, straight bore length, base metal and hardness, deposit or burr condition, required surface finish if any, and current speed or fixture type. Quantity matters as well because wire pipe brush life changes with the deposit. A brush that lasts 2,000 cycles on light rust may not survive 400 cycles on heavy scale, and that affects unit cost more than the brush price does.
Send those details and a drawing if available to [email protected] or call +86 1580 0932 713. We will confirm fill material, stem diameter and length, brush OD, trim length, and twist direction before sampling so the first article does not become another shelf trial.
Common Questions About Wire Pipe Brush Specification
Can a wire pipe brush remove heavy weld scale or only surface rust?
A wire pipe brush can remove heavy scale, but only when the fill diameter, density, and stem are raised to carry the load. Surface rust comes off with 0.20 mm carbon steel fill at moderate speed. Weld scale needs 0.35 mm or heavier fill, a shorter trim, and lower RPM because the tips must chip rather than skim. If the scale is thicker than about 1 mm, the brush will wear fast and a descaling spiral or mechanical descaling pass may be the better first step.
What determines whether I need carbon steel or stainless fill?
It depends on the pipe material and what ends up in the bore after cleaning. Carbon steel fill suits steel and cast iron, but it can leave fine steel particles that corrode on stainless or food contact surfaces. Stainless fill costs more and still removes rust from stainless and alloy tubes without introducing carbon steel residue. If the pipe is copper or aluminum, brass or nylon abrasive fill is safer than stainless because it cuts less into the soft wall.
Which speed should I run on a wire pipe brush in a hand drill?
The most common mistake we see is running the same RPM used for a sanding drum. Start low. For a wire pipe brush under 20 mm OD, 800 to 1,500 RPM is workable on light rust. For 25 to 50 mm OD, stay below 1,000 RPM and watch the stem near the collet. The right speed is the one where the fill does not stall, the stem does not whip, and the brush does not throw debris sideways. If the stem bends or heats, reduce speed and use a larger stem or shorter overhang.
What happens if the brush OD is too large for the pipe?
A small oversize condition is not harmless. The fill folds over instead of cutting, the stem absorbs high torque, and the brush fails at the pipe mouth. We size standard wire pipe brushes 3 to 5 mm over nominal ID for hard fill and closer to 1 to 3 mm for brass or nylon fill. If the brush is only slightly oversize but runs hard, the tube wall can score. If you are not certain of the ID tolerance, send the minimum ID from the drawing and we will confirm the brush OD against the actual pipe tolerance before ordering.
If you’re interested, check out these related articles:
how do you know about deburring brushes
the differences between inward and outward spiral brush
main features and applications of hx nylon cylindrical brush
honing brush a magic tool for flexible burr removal